
What Information Should a Complete Manufacturing RFQ Include?

Executive Summary: Manufacturing suppliers lose hundreds of engineering hours every quarter chasing missing tolerances, vague material grades, and ambiguous delivery timelines. A complete manufacturing RFQ standardizes critical commercial and technical requirements upfront, allowing estimation teams to qualify opportunities rapidly, protect margin accuracy, and eliminate multi-day email friction before production planning begins.
The Anatomy of a Complete Manufacturing RFQ
In custom machining, contract manufacturing, industrial automation, and engineered-to-order equipment, the Request for Quote (RFQ) is the fundamental commercial handoff between buyer and supplier. Yet across precision manufacturing and OEM supply chains, inbound RFQ quality varies wildly. Procurement teams frequently submit incomplete packets containing only top-level assembly drawings, missing revision controls, unspecified material tempers, and unstated quality inspection protocols.
When suppliers accept an incomplete request, engineering and sales teams inherit hidden labor costs. Senior application engineers spend billable hours acting as intake clerks—requesting native CAD files, asking for target batch releases, clarifying surface roughness expectations, and confirming incoterms. Understanding what a complete manufacturing RFQ must include transforms an industrial supplier from a reactive estimator into a high-velocity engineering partner.
Company Snapshot: How High-Mix Manufacturers Manage Inbound Demand
Contract manufacturers, CNC precision machine shops, and custom fabricators operate in high-mix, variable-volume environments. Their core business model relies on converting engineering intent into physical parts through multi-axis milling, turning, sheet metal fabrication, injection molding, or additive manufacturing.
Their primary customers include tier-1 automotive integrators, aerospace subcontractors, medical device OEMs, and industrial machinery builders. In these relationships, speed to quote is one of the highest predictors of win rate. According to industry procurement benchmarks, the first qualified supplier that submits a technically sound quote with guaranteed lead times wins the order more than 50% of the time. However, quoting speed cannot come at the expense of margin defense or feasibility review.
What the Company Sells and How Procurement Buys
Precision manufacturing suppliers do not sell catalog commodities; they sell specialized machine capacity, metrology precision, certified materials processing, and programmatic delivery guarantees.
When enterprise procurement specialists or design engineers buy custom parts, their purchasing flow involves multi-stage technical validation:
Design Freeze & File Export: The buyer finalizes 3D solid models and 2D engineering drawings with Geometric Dimensioning and Tolerancing (GD&T).
Specification Assembly: The buyer drafts a statement of work covering base metals, secondary finishes, heat treatments, non-destructive testing (NDT), and shipping terms.
Vendor Distribution: The buyer emails RFQ packages to preferred vendor lists or submits them through supplier portals.
Supplier Estimation: The supplier verifies manufacturability, machine spindle availability, tooling requirements, raw stock pricing, and outside vendor processing times.
Proposal & Award: The supplier issues a formal quote containing unit pricing tier curves, non-recurring engineering (NRE) charges, tooling lead times, and payment milestones.
The Business Problem: Incomplete RFQs and the Latency Trap
When inbound packets lack vital specifications, the entire quoting engine stalls. Industrial sales departments report three recurring bottlenecks:
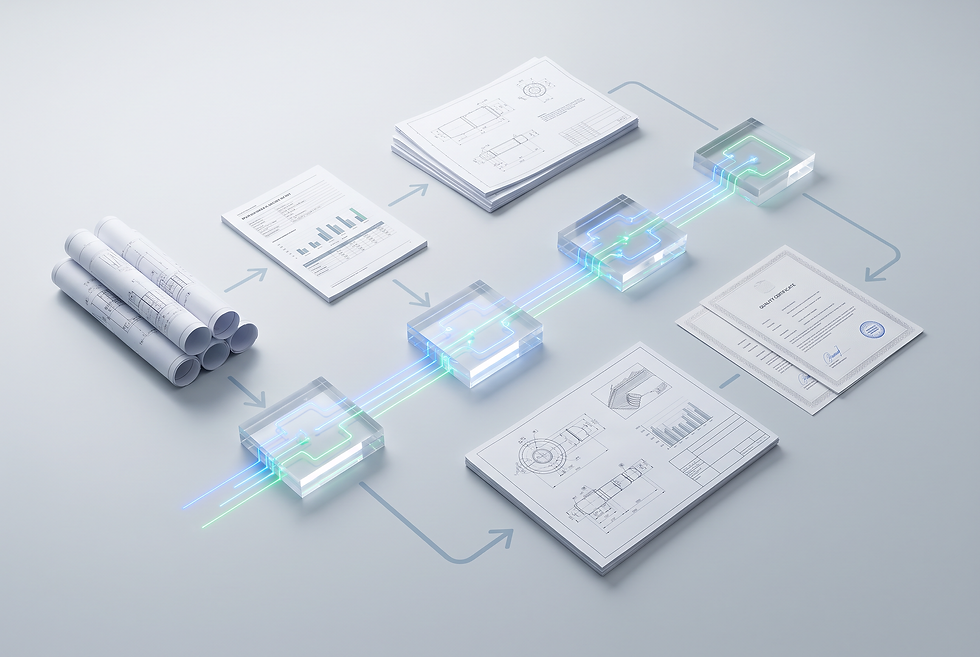
The Estimation Ping-Pong Cycle: Estimators cannot calculate cycle times without knowing whether a critical bore requires ±0.05 mm or ±0.005 mm tolerance. Clarification emails take 48 to 72 hours per loop, dragging response time past the evaluation window.
High-Value Engineering Drain: Senior manufacturing engineers spend up to 35% of their daily bandwidth reviewing unvetted inquiry files, answering basic revision mismatch questions, and deciphering corrupted files instead of optimizing toolpaths.
Margin Leakage and Misquoted Jobs: When assumptions are made on missing finish specs, packaging requirements, or material certs, suppliers underprice jobs or suffer unexpected subcontractor expenses during production.
What Changed: Structured Intake and Automated Qualification
Leading contract manufacturers and industrial equipment builders have shifted away from unstructured inbox-driven quoting. Instead of allowing raw emails to flood technical estimators, forward-thinking operations deploy systematic qualification frameworks and automated intake layers.
This operating model divides the RFQ review process into distinct layers: programmatic data extraction, automated completeness validation, rule-based commercial filtering, and human engineering sign-off. By requiring unambiguous inputs across 12 specific dimensions, suppliers eliminate missing data before estimation begins.
The 12 Core Elements of a Complete Manufacturing RFQ
To ensure an estimation team can quote accurately on the first pass, a complete manufacturing RFQ packet must contain the following twelve core parameters:
Company & Project Context: Buyer legal entity, primary engineering contact, procurement lead, project name, application environment, and lifecycle stage (prototyping, pilot run, bridge tooling, or steady-state serial production).
Part Application & Operating Environment: Operating temperatures, chemical exposure, vibration profiles, mechanical load constraints, and mated component relationships.
Design Files & Formats: 3D native CAD files (STEP, IGES, Parasolid) matched with vector 2D technical drawings (PDF/DWG) showing explicit datum structures and revision letters.
Material Specifications: Exact material grade and alloy designation (e.g., 6061-T6 Aluminum, 316L Stainless Steel, PEEK 450G), temper, raw stock form, and acceptable equivalent substitutions.
Tolerances & Critical Dimensions: General shop tolerances (e.g., ISO 2768-m) complemented by explicit GD&T callouts, surface profile limits, true position callouts, and highlighted Critical to Quality (CTQ) dimensions.
Volume & Batch Release Schedules: First article quantity, prototype batch size, estimated annual usage (EAU), blanket purchase order parameters, release cadence, and minimum batch sizes.
Surface Finish & Post-Processing: As-machined Ra values, bead blasting specifications, anodizing type and class (e.g., MIL-A-8625 Type III Hardcoat), electropolishing, passivating, powder coating RAL codes, or case hardening depth.
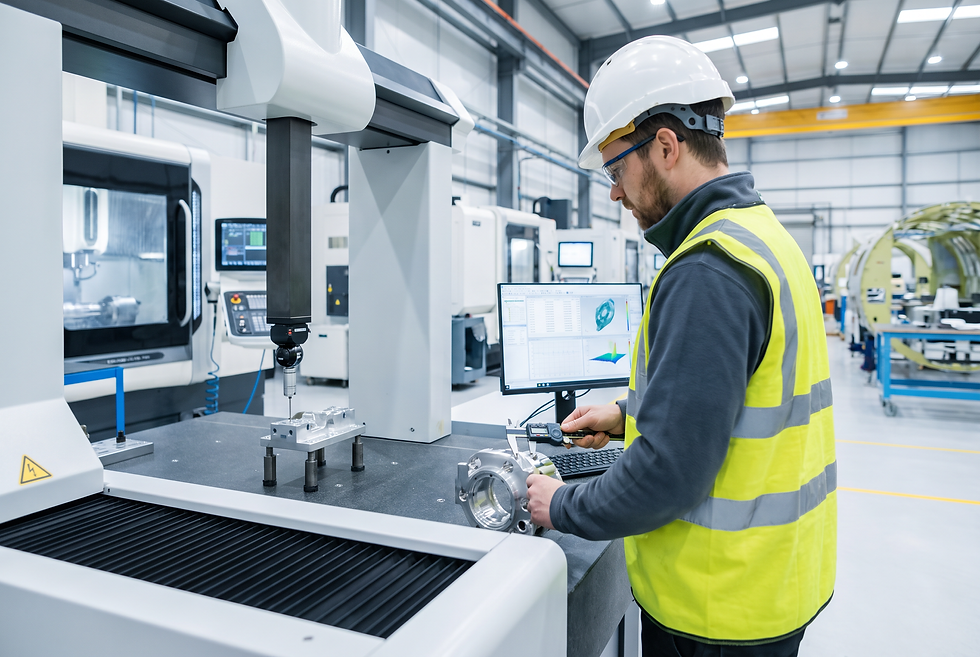
Quality Inspection & Metrology: First Article Inspection (FAI / AS9102), CMM inspection reports, material test reports (MTR), heat treat charts, plating thickness verification, and non-destructive testing requirements.
Compliance & Certifications: Industry standards including ISO 9001, AS9100, ISO 13485, IATF 16949, ITAR restrictions, RoHS/REACH compliance, and DFARS specialty metals compliance.
Delivery Timeline & Schedule: Prototype deadline, FAI submission target date, production run delivery dates, ramp-up schedules, and expedited freight conditions.
Commercial Terms & Target Pricing: Target piece-part budget, allowable tooling/NRE amortization, payment terms (Net 30/60, progressive milestones), and delivery terms (Incoterms 2020: EXW, FOB, DDP).
Decision Criteria & Purchasing Authority: Award decision timeline, single vs. multi-source strategy, technical versus commercial weighting, and designated commercial sign-off authority.
RFQ Dimension | Key Data Requirement | AI / Automated Intake Role | Human Engineer / Sales Role |
CAD & Drawings | 3D STEP + 2D PDF with matching rev levels | Validates file integrity, geometry formats, and rev consistency | Evaluates tooling accessibility, thin walls, and setup complexity |
Material & Temper | Precise alloy grade, standard, and mill cert spec | Cross-references alloy databases and flags obsolete callouts | Negotiates material substitutions and validates thermal stability |
Tolerances & GD&T | ISO 2768-m baseline + explicit CTQ tolerances | Parses title block tolerances and flags micro-tolerances (< ±0.005mm) | Confirms machine capability, fixture rigidity, and CMM metrology |
Volume & Schedule | Prototype batch, EAU, and release intervals | Calculates preliminary stock requirements and lead time bands | Evaluates capacity schedule, machine slots, and raw stock procurement |
Surface Finish | Mil-spec coating, Ra roughness, plating callouts | Identifies finishing callouts and queries outside processor lists | Solicits outside vendor quotes and determines masking complexity |
Quality & Compliance | AS9102 FAI, CMM reports, RoHS/REACH, ITAR | Verifies compliance clauses and export control flags instantly | Signs off on quality assurance plans and customer audit requirements |
Commercial Terms | Incoterms, target price, payment milestones | Validates credit limits, minimum order values, and incoterm rules | Approves final margin spreads, progressive invoicing, and liability |
How the Automated RFQ Qualification Workflow Actually Works
A modern intake workflow does not replace senior application engineers; it shields them from incomplete data packets. Here is how high-performance manufacturers execute this process across seven discrete steps:
Step 1: Multi-Channel Ingestion: Inbound inquiries enter through website intake forms, customer portals, or dedicated RFQ mailboxes. Files, text notes, and attached purchase agreements are ingested simultaneously.
Step 2: Automated Parsing & File Validation: The system parses PDF drawings, reads title blocks, checks for matching revision letters between 2D prints and 3D CAD files, and flags missing dimension sheets.
Step 3: Qualification & Gap Detection: The automated intake logic evaluates the submission against the 12 core criteria. If an essential parameter (e.g., surface roughness or material cert type) is missing, the system detects the gap in real time.
Step 4: Autonomous Clarification Request: Before an engineer reviews the file, the intake engine generates a precise clarification draft to the buyer specifying the exact missing details.
Step 5: Commercial Feasibility & Capability Triage: Once complete, the system evaluates part dimensions against machine envelope limits (e.g., max 5-axis travel, lathe bar capacity) and assesses export requirements.
Step 6: Human Application Engineering Review: The qualified, fully assembled packet is routed directly to the designated Application Engineer with an executive summary of critical tolerances, tooling notes, and stock availability.
Step 7: Rapid Quote Generation & Follow-Up: The sales representative issues a formal quote within hours rather than days. Automated tracking monitors proposal opens and triggers timely follow-up sequences.
Evidence and Results: What the Numbers Show
Adopting structured, qualified RFQ protocols delivers measurable operating improvements across precision manufacturing and technical sales environments:
Quoting Cycle Acceleration: According to industrial supply chain studies published by Thomas and benchmark data from the National Tooling and Machining Association (NTMA), suppliers with standardized digital intake cut RFQ response latency from an industry average of 4.8 business days down to under 24 hours.
Engineering Bandwidth Recovery: Manufacturing operations utilizing automated parsing and specification checklists report a 60% reduction in time spent by senior engineering staff chasing missing drawing metadata, as documented in published digital transformation case studies.
Higher Bid Win Rates: A benchmark published by the Precision Metalforming Association (PMA) indicated that contract suppliers delivering complete, compliant technical quotes within the first 24 hours capture up to a 40% higher contract win rate compared to late-responding competitors.
What Other Companies Can Learn: Replicable Operating Principles
Industrial businesses looking to modernize their technical sales pipeline should implement four foundational principles:
Standardize the Intake Threshold: Never allow an unvetted email to enter engineering review. Establish a rigid definition of a qualified RFQ and enforce it uniformly across web forms, distributor networks, and direct sales channels.
Separate Data Hygiene from Manufacturing Engineering: Application engineers are skilled problem solvers, not data entry clerks. Use automation to extract title block metadata, verify file revisions, and request missing parameters before human review.
Map Subcontractor Dependencies Early: Many quoting delays stem from third-party platers, heat treaters, and raw material distributors. Build instant pricing tables for standard finishes to eliminate outside vendor lag.
Maintain Continuous Lead-Time Transparency: Keep production schedules linked to quoting logic so sales reps never quote standard lead times when machine shop capacity is constrained.
What This Could Look Like for Industrial Equipment and Precision Machining
For an industrial machinery builder, custom pump manufacturer, or precision CNC supplier, applying this structured intake workflow transforms commercial throughput:
For a Precision CNC Machining Supplier: When a medical device manufacturer submits an RFQ for surgical titanium components, the automated intake instantly extracts GD&T tolerances, verifies ISO 13485 cleanroom requirements, checks raw bar stock availability, and requests missing passivation specifications before engineering programming review.
For a Packaging Machinery OEM: When a consumer packaged goods brand requests a custom carton-handling system, the intake engine cross-checks line speed requirements, power supply specs, conveyor clearance envelopes, and factory acceptance test (FAT) criteria, drafting an intake summary for the solutions architect.
For an Industrial Valve and Pump Manufacturer: When an EPC contractor submits an oil & gas bid, the system verifies ASME / API pressure ratings, flange dimensions, NACE MR0175 sour service compliance, and painting schedules, ensuring zero estimation omissions.
YTT AI Worker Mapping: Deploying the AI Business Development Rep
To operationalize this complete manufacturing RFQ framework without expanding non-technical administrative overhead, industrial manufacturers can deploy a dedicated autonomous digital employee.
AI Business Development Rep (Technical Sales & RFQ Intake)
Worker Job Title: AI Business Development Rep (Industrial & Precision Manufacturing)
Main Daily Tasks: Ingest inbound RFQs from web portals and email inboxes; parse technical drawings and BOMs; validate file formats and revision parity; identify missing technical parameters; draft instant clarification emails to buyers; score commercial and technical feasibility; route complete packets to application engineers.
Primary Work Channel: RFQ email inboxes, supplier portal webhooks, ERP/CRM systems, and internal engineering communication channels.
Authority Boundary: Can autonomously acknowledge receipt, request missing non-sensitive technical data, check stock availability, and log customer parameters. Cannot modify approved shop hourly rates, commit machine capacity without rules-engine approval, or issue binding contract signatures without commercial director sign-off.
First Value Event: Ingesting an incomplete 15-part RFQ package from a tier-1 customer, identifying two missing drawing revisions and an unstated anodizing spec, and autonomously sending a polite, formatted clarification email within 90 seconds of submission.
Daily Report Result: A structured summary delivered every morning to leadership detailing total RFQs received, fully qualified packets, autonomous clarifications pending, non-feasible bids rejected, total pipeline value quoted, and average intake-to-engineer velocity.
FAQ
What happens if a buyer submits an RFQ without 3D CAD files?
When an RFQ is submitted with only 2D PDF drawings, manufacturing estimators must manually recreate 3D geometry or perform manual mathematical step calculations to determine toolpaths and material volume. While standard parts can be quoted from detailed 2D drawings with full GD&T, 3D STEP or Parasolid files reduce estimation time by up to 80% and eliminate geometric misinterpretations.
Why is annual volume or batch release schedule critical in an industrial RFQ?
Manufacturing cycle times, raw material bulk discounts, and tooling strategies depend heavily on lot size. Quoting 50 prototype parts requires standard modular fixturing and single-piece setups, whereas a blanket order of 50,000 units with monthly releases justifies dedicated multi-cavity tooling, custom jaws, automated pallet pools, and aggressive volume pricing.
How does automated RFQ qualification prevent margin leakage?
Automated qualification scans the entire RFQ packet for hidden cost drivers such as specialized plating, non-destructive testing, certificate of conformance requirements, and strict packaging protocols. By surfacing these items before the quote is submitted, the sales team ensures all subcontractor costs and inspection overheads are accurately factored into the proposal price.
What is the difference between an RFI, RFQ, and RFP in manufacturing?
A Request for Information (RFI) evaluates a supplier's general technical capabilities and quality certifications. A Request for Quote (RFQ) focuses on specific pricing, lead times, and terms for well-defined part specifications. A Request for Proposal (RFP) asks the supplier to propose custom engineering concepts, system architectures, or technical solutions to solve a broad problem.
Standardize Your Technical Inbound Pipeline
Stop letting incomplete drawing packages and missing specs slow down your engineering team. Get the RFQ Qualification Checklist to streamline your intake, accelerate turnaround times, and protect production margins across every quote.


Comments