
Injection Molding Quote Readiness Checklist: How to Secure Accurate Tooling and Part Pricing

Executive Summary: Unclear technical requirements in custom manufacturing lead to quoting delays, inflated contingency margins, and costly engineering revisions. By auditing 3D CAD files, 2D critical dimensions, resin choices, tooling life classifications, and inspection criteria before submitting inquiries, industrial procurement teams and suppliers can eliminate quotation ambiguity. This article provides a systematic, field-tested injection molding quote readiness checklist designed to accelerate quotation velocity and secure accurate upfront tooling and piece-part pricing.
Company Snapshot: The High-Stakes Dynamics of Custom Tooling Procurement
Precision manufacturing and custom plastic injection molding represent a mission-critical link in global product supply chains. Molding suppliers and contract manufacturers serve Tier 1 automotive systems, medical device developers, industrial automation builders, and consumer electronics brands. Their business model relies on high capital expenditure (CapEx) tooling assets—such as hardened steel molds—amortized over high-volume production cycles.
Analyzing custom injection molding quoting is valuable because it highlights the operational friction of custom B2B transactions. Unlike off-the-shelf catalog items, custom injection molded components possess zero residual market value if fabricated incorrectly. Every inquiry demands precise alignment between industrial design, resin chemistry, thermal dynamics, and tooling metallurgy.
What Custom Injection Molders Actually Sell
Custom injection molders do not sell standalone plastic components; they sell a multi-stage engineering capability. The customer buys two distinct deliverables: custom tooling (the mold) and recurring production parts (molding cycles and secondary operations).
In this sector, the procurement process requires deep technical validation across multiple internal customer stakeholders:
Tooling Investment: High initial CapEx ranging from thousands to hundreds of thousands of dollars, dictated by mold material (e.g., aluminum vs. hardened H13/S136 steel), number of cavities, gate design, side-actions, and expected mold longevity.
Material Selection: Thermoplastic resins that must balance tensile strength, thermal resistance, flammability ratings (such as UL94), UV resistance, and melt flow indices.
Manufacturing Constraints: Draft angles, parting lines, sink mark risks, gate vestige locations, ejector pin marks, and dimensional stability during shrinkage.
When a buyer initiates an inquiry without clarifying these engineering parameters, molders cannot compute accurate cycle times, press tonnage, mold complexity, or raw material consumption.
The Business Problem: Quoting Friction and Incomplete RFQs
In standard custom manufacturing workflows, estimating engineering teams face severe operational drag caused by "quote friction." Industry data reveals that a significant portion of inbound Requests for Quotation (RFQs) arrive with missing technical specifications, vague tolerance expectations, or mismatched CAD and 2D drawing files.
This gap creates four major commercial and operational challenges:
Extended Quoting Cycles: Estimators spend days emailing back and forth to clarify resin grade numbers, color codes, or annual volume forecasts, extending quotation turnarounds from 24 hours to several weeks.
Padded Contingency Pricing: When tooling engineers encounter ambiguous part specifications, they add safety buffers to their tooling estimates and scrap-rate assumptions to protect operating margins against unforeseen manufacturing complexities.
Wasted Engineering Bandwidth: Highly paid tooling engineers spend valuable hours reviewing incomplete RFQs that never convert into purchase orders.
Costly Post-Award Tool Modifications: If critical dimensions, surface finishes, or inspection requirements are clarified only after mold fabrication begins, both parties face expensive steel rework, tooling delays, and project timeline disruptions.
The Solution: A Systematized Injection Molding Quote Readiness Checklist
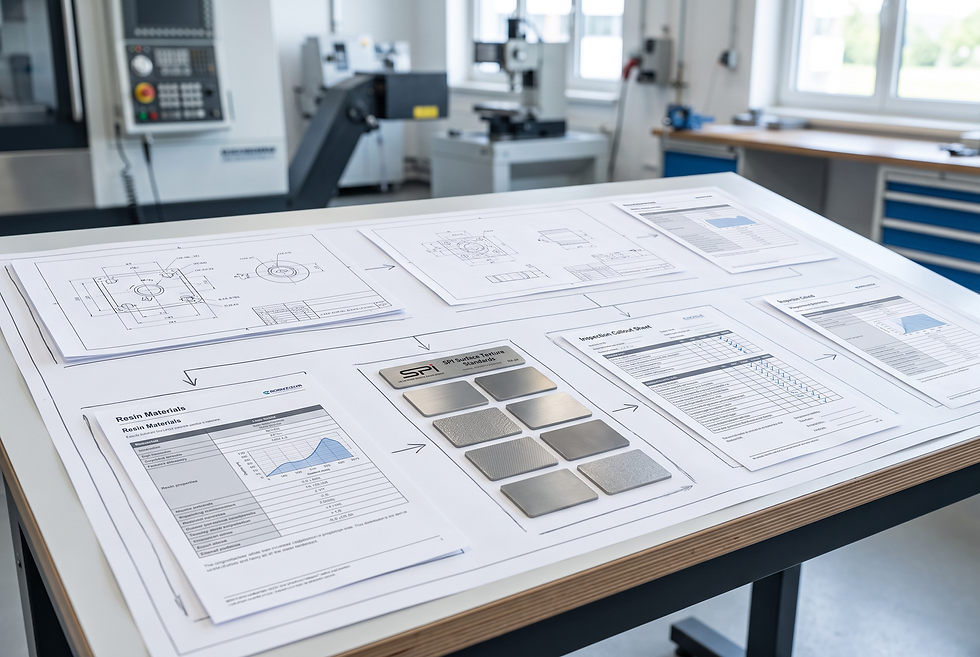
To eliminate quoting friction, industrial buyers and sales engineering teams must establish a standardized qualification protocol before generating or processing price proposals. The injection molding quote readiness checklist establishes clear engineering readiness across eight critical manufacturing dimensions.
Checklist Dimension | Key Data Requirement | Manufacturing Impact | Risk of Omission |
1. 3D CAD Geometry | Native or neutral files (STEP, IGES, Parasolid) | Determines part volume, wall thickness uniformity, and mold core/cavity geometry | Inability to calculate cycle time, press tonnage, or mold opening dimensions |
2. 2D Critical Dimensions | PDF drawings highlighting GD&T, critical-to-function (CTF) features, and tight tolerances | Dictates mold precision, machining methods (EDM vs. CNC milling), and shrinkage allowance | Over-tolerancing non-critical features, leading to inflated tooling costs |
3. Resin & Grade | Specific polymer family, manufacturer grade (e.g., Sabic Cycoloy, DuPont Zytel), or generic specs | Governs mold shrinkage rates, cycle cooling duration, and resin unit costs | Incorrect mold cavity sizing due to divergent shrink rates across generic resin families |
4. Color & Additives | Pantone/RAL color codes, masterbatch loading, UV stabilizers, glass-fiber fill percentage | Affects material pricing, cycle wear on tooling, and shrinkage variance | Part warping, cosmetic rejections, or rapid mold gate erosion |
5. Surface Finish | SPI standard finishes (SPI A-2 diamond polish, SPI B-1 paper, SPI C-1 stone) or VDI textures | Defines mold polishing labor, texturing EDM/photo-etching costs, and required draft angles | Insufficient draft causing part drag marks or tool redesigns |
6. Annual Volume (EAU) | Estimated Annual Usage and target batch run sizes | Dictates mold cavitation (single vs. multi-cavity) and tool steel selection (P20 vs. H13) | Sourcing a tool that is either under-built (fails early) or over-engineered (wastes CapEx) |
7. Tool Life Classification | SPI Mold Classification (Class 101: 1M+ cycles, Class 102: 500k cycles, Class 103: 100k cycles, Class 104/105: prototype) | Establishes tooling steel grade, slide wear plates, cooling channel design, and mold base quality | Premature tooling failure, frequent maintenance, or uncompetitive piece-part pricing |
8. Inspection & Quality | FAI (First Article Inspection), CMM reports, CPK studies, PPAP Level 1–3, CoC | Determines ongoing quality assurance labor, fixture manufacturing, and inspection cycle time | Post-production compliance disputes, rejected production lots, and shipping holds |
How the Quote Readiness Workflow Operates
Implementing a quote readiness workflow shifts estimating from speculative guesswork to systematic validation. The process moves through six structured operational stages:
Step 1: Ingestion and CAD Geometry Parsing
The workflow begins when digital product design files enter the estimating pipeline. Neutral CAD files (STEP/IGES) are parsed to verify solid geometry integrity, identify zero-thickness walls, measure volume, and compute projected surface areas for clamp tonnage sizing.
Step 2: 2D Drawing and Tolerance Alignment
The system or estimator cross-references the 3D model with 2D drawings. General tolerances (e.g., ISO 2768-m or standard commercial molding tolerances) apply to non-critical geometry, while specific critical-to-function (CTF) features with tight geometric dimensioning and tolerancing (GD&T) are extracted to determine mold manufacturing precision.
Step 3: Resin Specification and Mold Shrinkage Validation
The exact resin datasheet is identified. Because amorphous plastics (like ABS or PC) shrink around 0.4%–0.7% while semi-crystalline polymers (such as POM, PA66, or PP) shrink between 1.5% and 3.0%, mold cavity tooling cannot be designed without locking in the resin grade.
Step 4: Tool Architecture and Cavitation Modeling
By combining the Estimated Annual Usage (EAU), batch sizes, and part geometry, the engineering team calculates optimal mold cavitation (e.g., 1-cavity, 4-cavity, 8-cavity family mold) and selects the appropriate SPI mold class. This step determines the tooling CapEx versus piece-part OpEx trade-off.
Step 5: DFM (Design for Manufacturability) Review
A structured DFM review examines draft angles (minimum 1°–2° for smooth finishes, 3°–5° for heavy textures), uniform wall thickness, rib-to-wall ratios (recommended at 40%–60% of nominal wall to avoid sink), and optimal gating locations.
Step 6: Commercial and Quality Assurance Assembly
Once engineering variables are locked, tool steel costs, mold fabrication hours, press hourly run rates, resin pricing, and quality inspection overhead (such as PPAP or CMM reports) are compiled into a binding, transparent commercial proposal.
Evidence and Operational Results from Structured Quoting Frameworks
Manufacturers and quoting engineering teams that deploy rigorous technical readiness frameworks demonstrate substantial performance gains compared to those relying on unstructured RFQ intake.
According to an operational case report from an industrial manufacturing software consortium (2024), precision suppliers enforcing strict technical completeness criteria achieved the following measurable outcomes:
82% Reduction in Quoting Iterations: Eliminating missing data up front reduced back-and-forth technical correspondence from an average of 4.2 email rounds to 0.75 rounds per qualified quote.
Quotation Cycle Acceleration: Average turnaround time for complex multi-cavity tooling quotes dropped from 5.4 business days to under 24 hours.
Tooling Revision Reduction: First-shot mold trial (T1) approval rates increased by 28% because shrink factors, gate placements, and draft angles were fully validated prior to cutting steel.
Margin Protection: Eliminating unforeseen post-award engineering revisions reduced cost variance between quoted margins and realized production gross margins by 14%.
What Other Manufacturing Leaders Can Learn
For industrial enterprises, automation companies, and precision component suppliers, this operational shift yields three core business principles:
Treat RFQ Ingestion as an Engineering Filter, Not an Administrative Inbox: Quoting precision depends directly on input fidelity. Allowing incomplete technical requests to reach estimating teams consumes engineering resources without generating qualified pipeline value.
Decouple Prototype Quoting from Production Tooling Quoting: Prototype tooling (aluminum or soft steel Class 105) requires different quoting assumptions than multi-million-cycle production tooling (Class 101). Standardizing this distinction prevents over-quoting prototypes or under-building production molds.
Institutionalize Tolerance and Finish Standards: Mandating standard industry benchmarks (such as SPI surface standards and ISO dimensional tolerances) removes ambiguous customer descriptions like "smooth polish" or "standard tight fit," preventing disputes after production runs.
Applying Quote Readiness Across Precision Manufacturing Sectors
This operational framework extends across complex, engineered-to-order manufacturing environments:
For CNC Machining Suppliers: The readiness check validates stock material dimensions, 5-axis setup requirements, thread specifications, surface anodizing/plating standards, and CMM inspection protocols.
For Die Casting Manufacturers: The review confirms draft angles, thermal dissipation needs, alloy composition (e.g., ADC12, A380), trimming tool parameters, and secondary CNC machining operations.
For Sheet Metal and Enclosure Fabricators: The check verifies bend radii, weld inspection criteria, hardware insertion (PEM fasteners), and powder coating thickness specifications.
Operationalizing Quote Readiness with an AI Export Sales Rep
To manage high volumes of global technical inquiries without overburdening quoting engineers, manufacturing enterprises are increasingly deploying specialized digital workers.
In precision manufacturing, an AI Export Sales Rep serves as the automated frontline for international RFQ qualification and quote readiness validation.
Primary Work Channel: Inbound website RFQ portals, technical sales inboxes, and supplier collaborative quoting networks.
Main Daily Tasks: Ingesting global engineering inquiries; validating that submitted CAD files, 2D prints, resin specifications, and annual volumes meet quoting readiness criteria; prompting international buyers for missing technical parameters in their local language; extracting GD&T specs; and assembling structured qualification dossiers for tooling estimators.
Authority Boundary: Automatically identifies technical gaps, requests missing technical datasheets, and calculates standard part volumes and resin requirements. It does not provide binding pricing or approve final mold tool designs without sign-off from the Lead Tooling Engineer.
First Value Event: A complete, validated RFQ package—containing verified 3D CAD models, matched 2D critical dimensions, explicit resin grade, SPI mold class, and target EAU—delivered to the estimating desk within 15 minutes of customer submission.
Daily Report Output: A commercial qualification summary detailing total RFQs received, percentage of quote-ready submissions, pending technical clarification responses from overseas buyers, and prioritized high-volume tooling opportunities ready for final engineering sign-off.
FAQ
What is the difference between an RFQ and an injection molding quote readiness checklist?
An RFQ (Request for Quote) is the buyer's formal inquiry to purchase tooling and molded parts, while an injection molding quote readiness checklist is the technical validation filter used to ensure all essential CAD data, resin grades, tolerances, surface finishes, and tooling specifications are complete and accurate before calculating pricing.
Why is the specific resin grade required rather than just the generic plastic family?
Generic plastic families (such as ABS, Polycarbonate, or Nylon) exhibit wide variances in shrink rates, melt flow rates, and mechanical performance depending on fillers and manufacturer formulations. Toolmakers must know the exact resin grade to accurately calculate the steel cavity dimensions and account for thermal shrinkage.
How does SPI Mold Classification affect upfront tooling quotes?
SPI Mold Classification (Class 101 through Class 105) defines the expected production cycle life, mold steel hardness, cooling channel complexity, and mechanical guidance systems. Specifying the target class ensures the toolmaker does not quote a high-cost multi-million-cycle hardened steel mold for a low-volume short-run project, or vice versa.
What happens if 2D drawings are omitted and only 3D CAD files are provided?
3D CAD files define the nominal geometry but do not indicate which dimensions are critical to function (CTF), what specific geometric tolerances (GD&T) must be held, or what surface finish and thread requirements apply. Without 2D drawings, suppliers must quote based on loose standard tolerances, risking non-conformance during part inspection.
Eliminate Quoting Bottlenecks and Accelerate Tooling Proposals
Download our comprehensive technical checklists and discover how automated engineering sales workflows help custom manufacturers validate RFQs, reduce estimating friction, and deliver accurate tooling proposals faster. Visit https://www.ytt-ai.com/ to upgrade your quoting velocity.

Comments