
Manufacturing RFQ Qualification Checklist: What to Collect Before Quoting

Executive Summary: Unqualified Requests for Quotation (RFQs) create severe margin erosion and engineering bottlenecks across industrial supply chains. By establishing a systematic manufacturing rfq qualification checklist, custom fabricators, precision machine shops, and equipment manufacturers eliminate incomplete drawing submissions, triage commercial fit, and decouple estimation accuracy from manual engineering overhead. Implementing this operating model reduces preliminary quoting turnaround from business days to minutes while safeguarding engineering margins.
Operational Context: The Hidden Cost of the Unvetted Quote
In custom discrete manufacturing, precision machining, and industrial machinery, engineering capacity represents the tightest operational constraint. Application engineers and technical estimation teams spend dozens of hours every week manually reviewing engineering drawings, searching for missing geometric dimensioning and tolerancing (GD&T) callouts, confirming material availability, and back-and-forth emailing prospective buyers to clarify production volumes.
Industrial suppliers operate in a high-mix, variable-volume commercial model where quoting speed often correlates directly with win rate. However, accelerating response times without stringent qualification leads to catastrophic estimation errors, capacity misallocation, or unprofitable project commitments. Modern commercial operations address this challenge by shifting RFQ intake from passive inbox sorting to structured qualification.
What Custom Manufacturers Sell and How Commercial Friction Arises
Precision component suppliers, custom automated machinery builders, and contract manufacturers do not sell off-the-shelf catalog SKUs; they sell precision engineering capacity, metallurgy compliance, and production throughput. Every purchase order is initiated by an engineering packet comprising CAD models (STEP, IGES), 2D technical drawings (PDF, DWG), and commercial terms.
When a procurement officer or industrial buyer submits an RFQ, the transaction lifecycle depends on several interconnected operational criteria:
Design Manufacturability: Can the internal machine fleet (e.g., 5-axis CNC, sheet metal laser, EDM, robotic welding cells) execute the specified tolerances and tooling paths?
Material Sourcing Feasibility: Are specialized alloys, aerospace-grade billets, or food-grade polymers readily available through raw material distributors without excessive lead times?
Quality & Regulatory Governance: Does the job demand ISO 9001, AS9100, IATF 16949, or ISO 13485 certification, and does the client require Coordinate Measuring Machine (CMM) inspection reports, material test reports (MTRs), or first article inspections (FAIs)?
Commercial Alignment: Does the target production volume, batch cadence, and payment structure align with the manufacturer's gross margin floor?
When these twelve parameters are not validated upfront, estimation teams waste valuable technical hours chasing basic information or submitting blind estimates that later collapse in production.
The Business Problem: Quoting Chaos and Capacity Dilution
Traditional manufacturing sales operations suffer from three systemic process failures during RFQ intake:
Incomplete Engineering Submissions: Procurement portals and email inboxes routinely receive 2D prints lacking title blocks, missing surface finish specifications, or carrying conflicting tolerances between 2D drawings and 3D CAD models.
The Quoting Black Hole: Senior application engineers spend up to 40% of their working hours acting as customer service representatives, sending repetitive emails to clarify anodizing requirements, heat treatment specs, or delivery delivery dates.
Low Conversion on Low-Fit Inquiries: Commercial teams treat every RFQ with equal urgency, calculating detailed cycle times and tooling wear for one-off prototyping inquiries from buyers whose target pricing sits 50% below manufacturing cost.
To overcome these hurdles, commercial leaders require a standardized intake protocol that clearly defines what data must be captured before an RFQ enters engineering estimation.
The 12-Point Manufacturing RFQ Qualification Checklist
The following structured framework maps the essential parameters every industrial supplier must capture, categorizing the operational division of labor between automated intake systems and senior engineering authority.
# | Evaluation Dimension | Specific Data Required | Automation / Intake Role | Human Engineer / Sales Role | Operational Impact |
1 | Company Fit | Buyer domain, production niche, business registration, annual purchasing spend | Automated domain verification and CRM credit/enrichment lookup | Review strategic enterprise alignment | Filters out unauthorized hobbyists and non-commercial inquiries |
2 | Application Context | Operating environment (temperature, chemical exposure, load, industry sector) | Categorize application type via intake form or extraction | Validate extreme environmental risks or liability concerns | Prevents material degradation claims and warranty exposure |
3 | Technical Files | 3D native CAD (STEP/IGES) paired with 2D drawings (PDF/DWG) showing GD&T | Parse file formats, check file corruption, verify missing 2D/3D matches | Detailed manufacturability and internal toolpath assessment | Eliminates estimation pauses due to unreadable or missing CAD geometry |
4 | Material Specification | Exact alloy grade, hardness (e.g., 6061-T6, 316L, 4140 pre-hardened), raw billet vs. casting | Match grade against raw inventory catalog and distributor feeds | Approve non-standard exotic alloy substitutes | Avoids quoting obsolete or supply-constrained stock material |
5 | Tolerances & Critical Features | General linear tolerances (+/- 0.005" vs. +/- 0.0002"), true position, flatness callouts | Identify tight tolerance callouts (< 0.001") and flag inspection needs | Assess high-precision feasibility on existing machine axes | Protects against unachievable tolerances on standard shop machinery |
6 | Quantity & Order Cadence | Prototype batch vs. recurring production (EAU), delivery schedule (blanket PO) | Calculate quantity breaks and machine setup amortization | Validate machine scheduling and long-term cell capacity | Optimizes setup cost allocation and machine utilization |
7 | Surface Finish & Post-Processing | Ra values, anodizing (Type II/III), passivating, powder coat, heat treat, plating | Match standard finishing codes and calculate third-party vendor charges | Verify specialized coating specifications and masking drawings | Eliminates unexpected outside-processing (OP) markup costs |
8 | Inspection & Quality Control | CMM inspection, FAI (AS9102), dye penetrant, destructive testing, 100% optical inspection | Triage inspection tier and calculate standard QA labor hours | Senior QC manager confirms lab equipment and probe reach | Accurately factors metrology labor into the final price matrix |
9 | Certifications & Compliance | ITAR, DFARS, RoHS, REACH, Conflict Minerals, ISO standards, Material Test Reports | Filter export restrictions and regulatory checkmarks automatically | Sign off on defense/medical regulatory liability | Prevents severe legal non-compliance and export violations |
10 | Target Delivery Timeline | Required ship date, port of entry, expediting requirements, packaging standards | Compare lead time against raw material procurement cycles | Logistics director authorizes overtime shifts or air freight | Prevents contractual late delivery penalties (liquidated damages) |
11 | Budget & Target Pricing | Customer target piece price, tooling budget, previous historical benchmark | Collect target pricing to evaluate margin feasibility immediately | Determine commercial discounting and strategic pricing strategy | Prevents spending hours estimating bids doomed to commercial rejection |
12 | Decision Authority & Buying Process | Technical specifier vs. procurement sign-off, decision timeline, payment terms | Identify buying committee contacts and credit history | Direct outreach to engineering leadership vs. purchasing agent | Shortens the close cycle by engaging economic buyers directly |
How the Automated RFQ Qualification Workflow Actually Operates
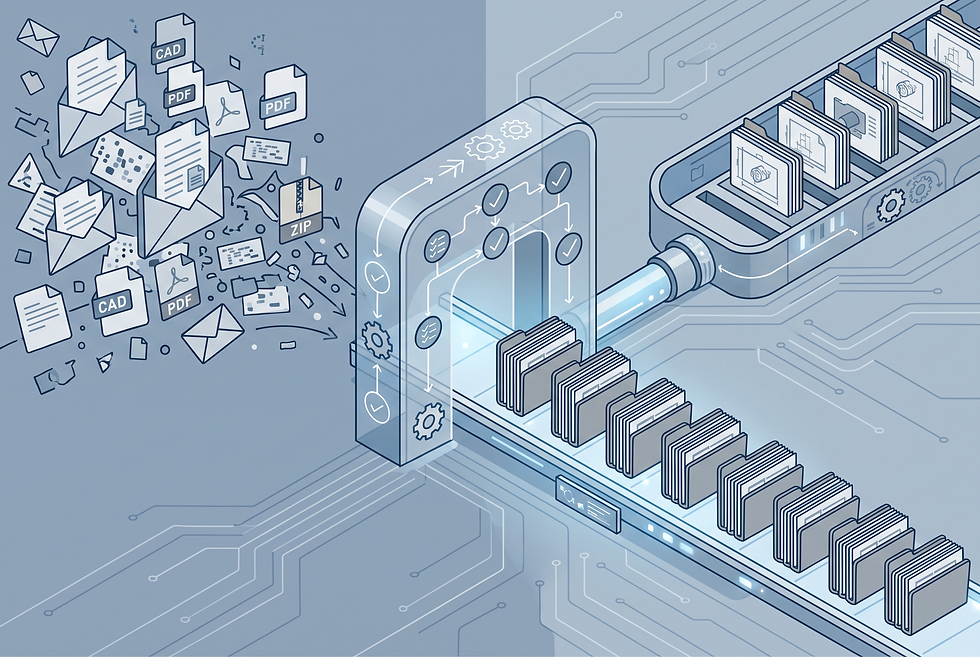
Adopting a modern manufacturing rfq qualification checklist does not mean turning away business; it means implementing a multi-stage validation workflow that collects technical parameters before high-cost manual work begins.
Step 1: Multi-Channel Data Ingestion
Inquiries arriving via email, contact forms, or electronic data interchange (EDI) are ingested centrally. Drawing packages containing zipped CAD models, PDF prints, and customer specifications are cataloged without manual intervention.
Step 2: Automated Technical Extraction and Pre-Flight Check
Before an application engineer opens the CAD file, the intake system scans the submission against basic manufacturability requirements. It verifies that 2D prints accompany 3D models, scans the text layer for critical alloy designations, and flags missing tolerances or non-standard surface treatments.
Step 3: Commercial Triaging and Fit Scoring
The account profile is verified against internal customer relationship management (CRM) records and industrial credit registries. If the company operates in a target vertical (e.g., medical device instrumentation or aerospace flight hardware) and satisfies minimum order volume thresholds, it is marked as high-priority.
Step 4: Automated Parameter Clarification
If a drawing submission lacks material callouts or specifies conflicting thread pitches, the system triggers an immediate clarification request to the buyer. This conversational clarification loop secures missing technical parameters while the RFQ is still fresh in the buyer's mind, saving days of manual back-and-forth.
Step 5: Human Engineering Authorization and Final Pricing
Once the 12-point manufacturing rfq qualification checklist is 100% complete, the estimating engineer receives a clean, vetted project brief. With all raw material prices, surface finish sub-tier quotes, and GD&T requirements clearly visible, the engineer calculates cycle times and issues a binding commercial proposal in hours rather than weeks.
Operational Results from Structured RFQ Workflows
Manufacturers that shift from unstructured inbox quoting to disciplined qualification mechanisms document consistent operational improvements across key commercial performance indicators:
Turnaround Speed: Industrial suppliers deploying structured intake workflows report accelerating first-response quoting times from an industry average of 4–6 business days down to under 4 hours for standard geometries, directly driving higher customer capture rates.
Engineering Capacity Reclamation: Eliminating manual document verification and missing-spec back-and-forth returns 15 to 25 hours per week of dedicated engineering time back to production floor optimization and high-margin custom design.
Margin Protection: Pre-flighting outside processing costs, strict inspection criteria (such as 100% CMM sampling), and non-standard raw alloy scrap rates prevents post-award margin slippage.
Strategic Principles for Industrial Sales Leaders
To replicate these operational efficiencies across discrete manufacturing and industrial equipment enterprises, commercial executives must enforce three core principles:
1. Treat Unqualified RFQs as Operational Friction, Not Sales Pipeline
An bloated sales pipeline filled with incomplete drawings and ambiguous quantities creates an illusion of commercial vitality while exhausting engineering resources. Enforcing strict gating criteria preserves estimating capacity for buyers ready to execute purchase orders.
2. Decouple Parameter Collection from Human Labor
Capturing material hardness, delivery addresses, and CAD formats does not require an advanced degree in mechanical engineering. Routine information gathering should be handled through standardized digital intake channels and automated conversational workflows, preserving human talent for design-for-manufacturability (DFM) analysis.
3. Establish Transparent AI and Engineering Authority Boundaries
While automated systems excel at file intake, standard alloy matching, and CRM data enrichment, final pricing approvals, custom tooling path sign-offs, and critical tolerance reviews must remain firmly under experienced engineering authority.
What This Looks Like for Equipment & Machinery Manufacturers
For industrial machinery builders, automated packaging line suppliers, and precision hydraulic valve manufacturers, RFQ intake often involves complex engineering specifications rather than simple machined parts.
In this environment, the manufacturing rfq qualification checklist shifts focus toward project integration parameters:
Plant Utilities and Spatial Footprint: Floor space dimensions, pneumatic line pressures, and voltage standards (480V 3-phase vs. 230V).
Throughput and Payload Requirements: Cycles per minute, maximum payload weight, and operational duty cycle.
Integration Interfaces: Upstream and downstream conveyor speeds, communication protocols (EtherNet/IP, PROFINET, Modbus), and safety cell certifications.
When these systemic requirements are gathered during initial intake, mechanical design leads can immediately assess engineering scope without conducting multiple preliminary discovery calls.
Deploying AI Workers in Industrial Commercial Operations
To execute this operating model at scale, modern industrial manufacturers deploy specialized, purpose-built AI workers that manage the entire front-end commercial workflow.
Target Role: AI Technical Sales Rep
Primary Daily Tasks: Ingest inbound RFQ emails and web inquiries 24/7, parse incoming technical drawings and specification sheets, cross-reference part dimensions against internal machine capability matrices, and initiate conversational clarification for missing checklist parameters.
Primary Work Channels: Corporate email inboxes, supplier portal webhooks, and enterprise CRM/ERP systems.
Authority Boundaries: The AI Technical Sales Rep is strictly authorized to qualify leads, gather missing CAD/GD&T parameters, calculate standard lead-time estimates based on live material distributor feeds, and draft quotation summaries. It is not authorized to grant custom margin discounts, alter contractual liability clauses, or issue binding bids on non-standard alloys without human engineering sign-off.
First Value Event: Successfully receiving a multi-part RFQ package with missing tolerance data, automatically securing the updated 2D PDF print from the buyer within 15 minutes, and delivering a fully enriched, production-ready estimating packet directly to the Chief Estimator.
Daily Operational Report: Summarizes total inbound RFQs triaged, complete vs. incomplete drawing packages, top missing parameters across submissions, average qualification turnaround times, and high-priority RFQs queued for senior engineering review.
FAQ
Why is a manufacturing RFQ qualification checklist essential for industrial suppliers?
A structured qualification checklist prevents engineering teams from wasting hours on unvetted, incomplete drawing packages. By verifying material availability, GD&T callouts, compliance certifications, and commercial fit before quoting, manufacturers protect profit margins and shorten turnaround times.
What are the most common missing parameters in manufacturing RFQs?
The most frequently omitted parameters include exact material grades (e.g., specifying 'aluminum' instead of '6061-T651'), critical surface finish Ra callouts, inspection requirements (such as CMM or First Article Inspection), and realistic annual usage quantities (EAU).
How do manufacturers handle 2D drawings that conflict with 3D CAD models?
Best practice dictates that the 3D model governs basic geometry while the 2D drawing governs critical tolerances, GD&T callouts, surface roughness, and thread specifications. When discrepancies occur, automated intake workflows flag the mismatch for immediate buyer clarification before estimation begins.
Can automated AI workflows handle technical manufacturing qualification safely?
Yes, provided clear authority boundaries are established. Automated AI systems handle file pre-flighting, missing parameter collection, and CRM logging, while human application engineers maintain sole authority over manufacturability approvals, machine toolpath feasibility, and final pricing sign-offs.
Standardize Your RFQ Qualification Workflow
Download our comprehensive industrial qualification toolkit or connect with our technical sales specialists to automate intake, eliminate drawing bottlenecks, and accelerate your quoting speed.


Comments