
Tooling Supplier Risk Assessment Guide: 10 Questions to Ask Before Awarding

Executive Summary
Global manufacturing procurement teams often face severe margin erosion from injection mold fabrication delays, hidden engineering changes, and unverified steel certifications. This case study examines how industrial program managers restructured vendor qualification across tool design, Moldflow validation, steel provenance, and production readiness. By implementing an objective assessment framework, procurement organizations reduce engineering change orders, ensure on-time T1 sampling, and protect proprietary part geometry across international supply chains.
Company Snapshot: High-Precision Industrial Tooling Procurement
Precision tooling procurement represents one of the highest capital expenditure risks for original equipment manufacturers (OEMs), automotive Tier-1 suppliers, and industrial automation enterprises. In complex assembly environments, a single tooling failure—whether caused by improper thermal layout, suboptimal hot runner selection, or uncertified mold steel—cascades into assembly line shutdowns and costly launch delays.
Industry: Industrial Machinery, Automotive Components, and Precision Enclosures.
Core Sourcing Category: Multi-cavity injection molds, high-pressure die casting dies, and precision stamping tools.
Primary Stakeholders: VP of Global Sourcing, Tooling Program Managers, Lead Mechanical Engineers, and Export Directors.
Business Model: High-mix, medium-to-high-volume component manufacturing requiring tight dimensional tolerances (ISO 2768-mK or tighter).
Analytical Focus: The operational shift from evaluating tooling quotes purely on piece-part price to rigorous technical risk scoring across pre-award engineering and manufacturing validation.
What Tooling Buyers Procure and the Inherent Commercial Risks
Procuring an industrial injection mold is fundamentally distinct from transactional commodity purchasing; it is an extended engineering collaboration. Tooling buyers contract for dedicated manufacturing assets that must produce millions of defect-free parts under continuous thermal, mechanical, and rheological stress.
The tooling procurement lifecycle involves distinct phases: preliminary part design review (DFM), mold flow simulation, tool steel procurement, CNC roughing and finishing, EDM sparking, hot runner integration, mold assembly, and trial sampling (T0, T1, to PPAP validation).
Because production molds frequently cross international borders before entering mass production, defects identified late in the build cycle cause exponential cost multipliers. Correcting cooling channel imbalances, gate blush, or ejector pin interference at the buyer's domestic plant costs significantly more than resolving design flaws during preliminary CAD sign-off.
The Business Problem: Latent Vulnerabilities in Traditional RFQs
Traditional request-for-quote (RFQ) workflows create blind spots for commercial buyers. Sourcing managers frequently select suppliers based on aggressive initial lead times and competitive pricing, only to encounter chronic execution failures during fabrication.
Unverified Steel and Component Provenance: Vendors quote premium European or Japanese mold steels (such as Böhler, Uddeholm, Daido, or Assab 1.2343/1.2738) but substitute lower-grade domestic equivalents without authentic mill test certificates, leading to premature mold wear, parting line collapse, and stress cracking.
Superficial Moldflow Simulations: Suppliers run automated Moldflow reports as marketing collateral rather than actionable thermal and rheological analyses, failing to predict weld lines, air traps, volumetric shrinkage, and sink marks.
Unclear Tool Ownership and Maintenance Rights: Inadequate contractual clarity around intellectual property, tooling wear-and-tear liabilities, and spare part interchangeability creates operational bottlenecks when tools are transferred to contract manufacturers.
Communication Gaps During Tool Build: Weekly status reports often mask design iteration bottlenecks, leaving buyers unaware of T1 sampling slips until critical production milestones have passed.
What Changed: Moving to an Engineering-First Qualification Framework
To mitigate multi-million dollar program risks, leading industrial buyers and export manufacturers transitioned from price-based supplier bidding to an integrated technical risk audit. Rather than relying on high-level vendor claims, sourcing teams implemented a structured tooling supplier risk assessment guide that enforces verifiable technical checkpoints prior to releasing tooling deposits.
Instead of evaluating only commercial terms, sourcing teams established structured verification checkpoints across ten mission-critical operational pillars before releasing tooling advances.
How the Tooling Supplier Risk Assessment Guide Operates in Practice
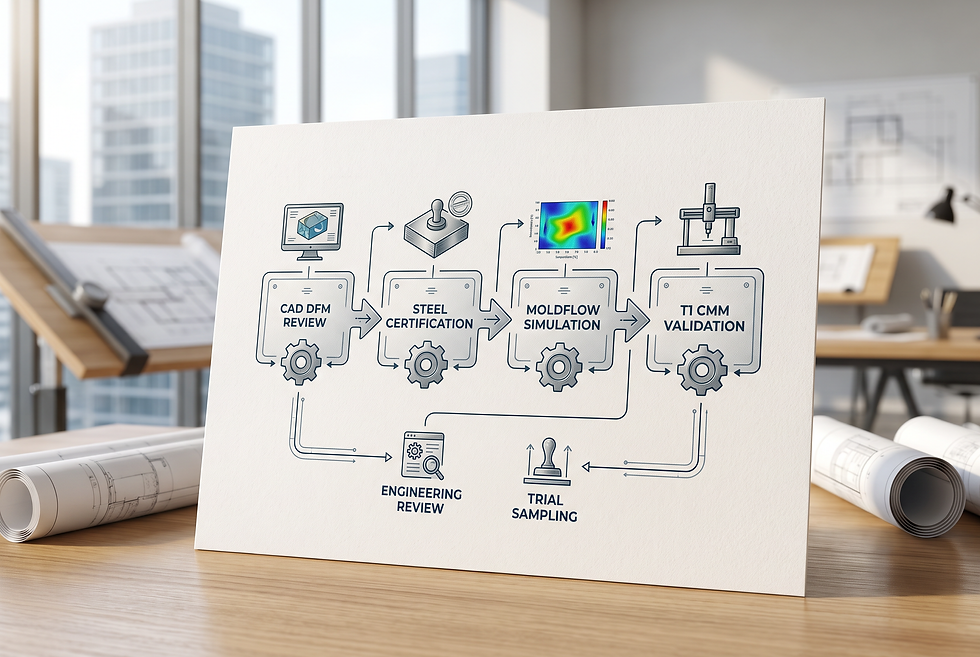
A robust supplier qualification workflow consists of six sequential verification gates that ensure accountability before, during, and after contract execution.
Step 1: Pre-Award DFM and Design Capability Audit
Before awarding the mold program, the buyer requires a detailed Design for Manufacturing (DFM) package. The vendor's engineering team must demonstrate parting line strategy, slide and lifter mechanics, draft angle allocations, and ejector pin placement without ambiguity.
Step 2: Certified Raw Material and Component Traceability
The supplier must submit verifiable Mill Test Certificates (MTC) with heat numbers for core, cavity, and mold base steels. Hot runner systems (e.g., Mold-Masters, Yudo, Synventive, Husky) and standardized mold components (e.g., HASCO, DME, Meusburger) must be backed by original distributor certificates.
Step 3: Rheological and Thermal Validation (Moldflow Review)
The mold builder performs comprehensive fill, pack, cool, and warp simulations using verified resin data sheets. Gating location, cooling circuit Reynolds numbers (>10,000 for turbulent flow), and volumetric shrinkage predictions must be formally reviewed and approved by both engineering leads.
Step 4: Program Management Milestone Tracking
Tooling builders implement gated milestone tracking tied to photographic, CMM, and video evidence at steel cutting, EDM completion, benching, and final fitting. This prevents self-reported progress estimates from masking fabrication delays.
Step 5: Structured Sampling Protocol (T0, T1, to PPAP)
The vendor executes trial sampling under specified resin drying and injection molding process parameters. T1 samples must include full dimensional inspection reports (FAIR), CMM data, mold temperature sensor logs, and cycle time verification against contract specifications.
Step 6: Tooling Asset Preservation, IP, and Export Readiness
Before sea or air shipment, the supplier applies protective anti-rust coatings, provides complete 2D/3D as-built mold drawings, electrode drawings, spare inserts, wear-plate specifications, and guarantees tool ownership release documentation without liens.
The 10 Critical Questions for Tooling Supplier Risk Assessment
Engineering and sourcing executives should evaluate suppliers against these ten foundational questions prior to contract award:
Tool Design & CAD Rigidity: Does the supplier maintain full-time in-house tooling designers, and do they design to DME/HASCO metric standards with complete 3D assembly models?
Steel Sourcing & Certification: What verifiable documentation (Mill Test Certificates, hardness testing logs) confirms the grade and heat treatment of core, cavity, and insert blocks?
Hot Runner Engineering: Is the manifold system engineered directly with the hot runner OEM, and does the thermal profile ensure uniform gate balance across all cavities?
Simulation Depth: Does the Moldflow simulation account for actual machine clamping tonnage, injection pressure limits, venting placement, and dynamic cooling turbulence?
Machining Precision & Tolerancing: What is the verifiable shop floor tolerance capability for high-speed CNC milling, wire EDM, and optical profile grinding on hardened steel?
Sampling Equipment Match: Are trial sampling presses comparable in platen dimensions, barrel capacity, screw geometry, and controller capability to the final production machines?
Validation & CMM Reporting: Does the vendor provide full-cavity CMM dimensional inspection and process capability studies (Cp/Cpk) on critical-to-quality (CTQ) dimensions at T1?
Preventative Maintenance Planning: What is the guaranteed shot life of the tool, and does the final delivery package include a scheduled spare-parts replacement list and wear-plate schematics?
IP & Asset Ownership: Does the supply agreement explicitly secure unencumbered buyer ownership of the mold, CAD data, and physical tooling assets without relocation penalties?
Program Communication & Escalation: How are technical engineering changes (ECOs) quoted, tracked, and verified across time zones during active fabrication?
Applying this comprehensive tooling supplier risk assessment guide enables procurement teams to uncover hidden capacity bottlenecks and evaluate suppliers on objective engineering rigor rather than speculative sales promises.
Evidence and Results: Quantifiable Impact of Structured Audits
Empirical data from manufacturing procurement audits demonstrates that upfront technical qualification yields substantial operational and financial gains.

According to an industrial manufacturing benchmarking study published by the Tooling & Sourcing Association (2024), companies implementing rigorous pre-award engineering reviews achieved measurable cycle improvements:
Assessment Area | Traditional RFQ Workflow | Structured Risk Audit Framework | Operational Impact |
Steel Verification | Self-reported invoice line | Independent Mill Test & Hardness Certificate | 88% reduction in premature core wear |
DFM / Moldflow Review | Basic gate recommendation | Complete thermal & warp simulation review | 42% decrease in post-T1 Engineering Change Orders |
T1 Sampling Accuracy | 62% on-schedule rate | 91% on-schedule rate with verified CMM | Average 3.2 weeks saved on production launch |
Cycle Time Compliance | +/- 18% variance from quote | Within 3% of target cycle time | Direct piece-part cost predictability |
IP & Asset Relocation | Frequent IP transfer friction | Contractual asset release with complete as-builts | Zero legal dispute friction upon mold transfer |
What Other Companies Can Learn: Transferable Sourcing Principles
Industrial organizations evaluating high-stakes capital purchases can adopt four strategic principles from this qualification model:
Separate Commercial Negotiation from Technical Auditing: Never finalize commercial terms before technical leads sign off on tooling architecture, steel selections, and cooling layouts.
Tie Financial Milestones to Physical Verification Gates: Disburse milestone payments (e.g., 30% deposit, 40% T1 sample approval, 30% final acceptance) strictly upon verified CMM reports, video documentation, and dimensional buy-off.
Standardize As-Built Documentation Standards: Require suppliers to deliver final 3D CAD models that reflect all manual fitting adjustments made on the bench prior to shipping.
Audit Machine and Tooling Compatibility: Ensure the supplier’s mold design aligns with the dry cycle, platen dimensions, tie-bar spacing, and ejection stroke of the designated mass-production press.
What This Could Look Like for Industrial Tooling and Precision Manufacturing
For precision mold manufacturers and global export suppliers, buyer scrutiny represents a powerful competitive differentiator. Forward-thinking tooling shops do not simply send static PDF quotes; they demonstrate structured engineering governance from the first customer touchpoint.
When a European or North American buyer issues an RFQ for a multi-cavity automotive connector mold, the export supplier's commercial and engineering teams must coordinate rapidly. They need to analyze 3D CAD files, formulate comprehensive DFM insights, validate steel availability, and communicate complex technical trade-offs across multiple time zones without days of delay.
Operationalizing Technical Response with YTT AI Workers
Scaling an engineering-intensive sales and qualification workflow requires substantial internal coordination. Tooling manufacturers and industrial exporters can deploy dedicated autonomous digital personnel to handle rigorous customer data exchanges.
Recommended Deployment: AI Technical Sales Rep
For custom tooling and mold manufacturing exporters, the most direct operational mapping is an AI Technical Sales Rep configured specifically for industrial tooling programs.
Main Daily Tasks: Ingests complex customer RFQ packages, checks 3D STEP/IGES files against baseline DFM rule sets, extracts critical-to-quality (CTQ) dimensional parameters, and assembles structured technical pre-qualification questionnaires.
Primary Work Channel: Technical email correspondence, B2B procurement portals, and integrated CRM communication streams.
Authority Boundary: Operates autonomously on technical data extraction, DFM preliminary checklists, and initial risk questionnaires; escalates custom hot runner calculations and binding commercial pricing to senior tooling engineering directors.
First Value Event: Automatically generating a standardized, bilingual 10-point Pre-Award Tooling Risk Audit & DFM Summary within 4 hours of customer CAD package upload.
Daily Report Result: A structured overview detailing new RFQs analyzed, identified tooling design ambiguities, outstanding supplier-buyer clarifications, and pending qualification milestones across active customer programs.
FAQ
What is the most critical question in a tooling supplier risk assessment?
While all technical parameters are vital, verifying steel provenance through authentic Mill Test Certificates (MTC) and rigorous hardness testing logs is paramount. Substandard or unhardened core and cavity steel causes premature thermal fatigue, dimensional drift, and catastrophic mold failure during mass production.
How does early Moldflow analysis reduce total tooling program costs?
Comprehensive Moldflow simulation identifies cooling channel imbalances, air traps, weld lines, and differential shrinkage prior to steel cutting. Resolving these issues in CAD prevents expensive post-T1 mold modifications, electrode EDM rework, and launch schedule slippage.
Why should milestone payments be linked to technical validation gates?
Structuring payments across verified gates (e.g., steel certification, T1 CMM dimensional approval, PPAP sign-off) ensures commercial alignment and guarantees that the supplier resolves all dimensional non-conformances before receiving final tooling disbursements.
What documentation should a buyer receive before a mold ships?
Buyers should receive final as-built 3D CAD files, 2D component drawings, electrode data, complete CMM inspection reports, machine trial parameter sheets, hot runner wiring schematics, spare insert lists, and an unencumbered mold ownership release certificate.
Standardize Your Tooling Qualification Process
Protect your capital expenditure and reduce launch delays by deploying structured technical risk assessments across your global injection tooling supply chain. Get the Tooling Buyer Scorecard at https://www.ytt-ai.com/ and streamline your supplier qualification workflow.


Comments